Choosing the best Enameled Aluminum Magnet Wire type in 2026 requires more than comparing conductivity figures. The right choice depends on motor design, operating temperature, winding space, insulation demands, and production conditions. A wire that performs well in a compact fan motor may fail to suit a high-load industrial transformer.
In practical winding evaluations, engineers usually examine conductor diameter, enamel thickness, thermal class, flexibility, and resistance stability. Aluminum offers lower weight and cost than copper, but it also requires careful joint design and tighter process control. Poor connections can create local heating. That detail is easy to overlook.
This guide compares common Enameled Aluminum Magnet Wire types used in modern motors, transformers, generators, and vehicle systems. It considers polyester, polyesterimide, polyamide-imide, and other insulation combinations. Each coating brings different benefits. Some tolerate higher temperatures, while others provide better abrasion resistance or improved chemical stability.
Real performance depends on more than a datasheet. Winding tension, storage humidity, stripping methods, and impregnation quality can change results. Small production errors matter. Even experienced teams may disagree about the “best” type, because application priorities differ. That uncertainty deserves attention.
The discussion follows established electrical-material principles and practical selection criteria. It does not treat one wire as universally superior. Instead, it explains where each type fits, what limitations engineers should verify, and which specifications deserve closer testing in 2026. Readers should confirm final choices through supplier documentation, sample winding trials, and relevant industry standards.
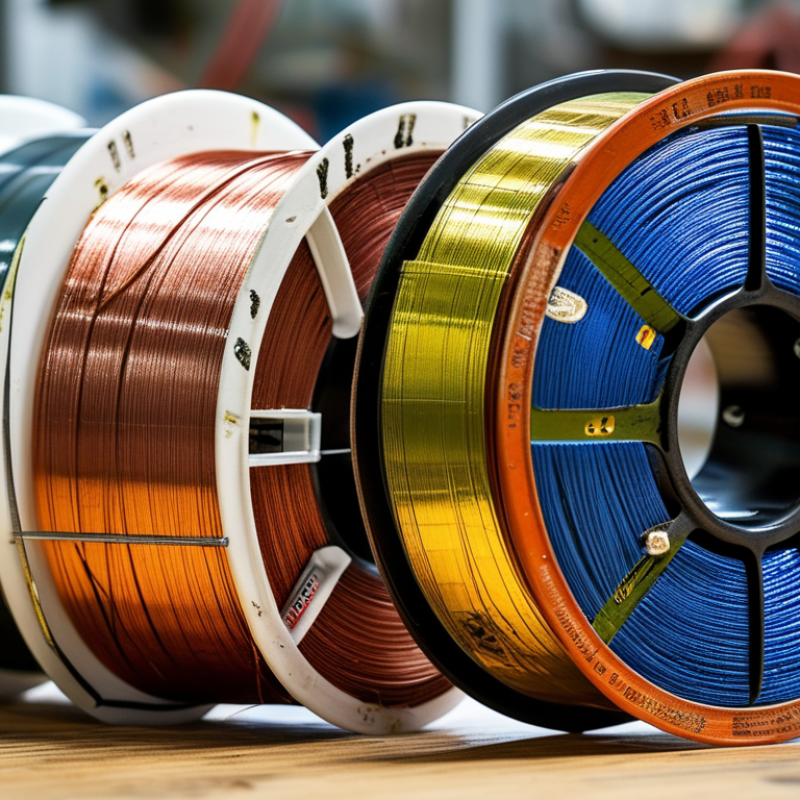
Enameled aluminum magnet wire is an aluminum conductor covered by a thin electrical insulation system. Its basic structure has three layers: the aluminum core, an enamel coating, and sometimes a bonding or protective topcoat. The core carries current, while the enamel prevents turn-to-turn contact inside motors, transformers, and coils.
The material choice has a clear physical reason. The Aluminum Association reports a density of about 2.70 g/cm³ for aluminum, compared with approximately 8.96 g/cm³ for copper. Aluminum is much lighter. Yet its conductivity is lower, usually near 61% IACS for electrical-grade aluminum, according to ASM Handbook data. Designers must therefore increase the conductor’s cross-sectional area. That trade-off is easy to underestimate.
IEC 60317-0-3 defines general requirements for enamelled round aluminum wire. Common insulation systems include polyesterimide and polyamide-imide. The first layer provides electrical insulation and heat resistance; the second can improve abrasion, solvent, and thermal performance. Round wire suits compact windings, while rectangular wire can improve slot utilization. Self-bonding coatings may hold a coil’s shape after controlled heating. Useful, but not always necessary. Testing should cover resistance, dielectric strength, flexibility, thermal aging, and coating adhesion. The IEC specification supports consistency, although real equipment still demands application-specific validation.
Choosing the best enameled aluminum magnet wire in 2026 requires more than comparing conductivity figures. The right type must match the motor, transformer, or coil’s actual working conditions. Start with conductor diameter and resistance tolerance. Small variations can change winding temperature and efficiency. Thermal margin matters.
Insulation performance deserves close attention. Check the thermal class, dielectric strength, flexibility, and resistance to abrasion. A wire may pass a voltage test yet crack during tight winding. That failure often appears later, under heat and vibration. Pay attention to elongation and enamel adhesion. These details support reliable production, especially when automatic winding equipment applies uneven tension.
Environmental exposure also influences selection. Moisture, oil vapor, refrigerants, and repeated temperature cycling can weaken unsuitable insulation. Request documented test data, including breakdown voltage, pinhole detection, and thermal aging results. Independent verification is more useful than a polished specification sheet. In practical evaluations, I would compare samples from the same production lot, then inspect them after winding and heat treatment. This approach reveals problems that catalog values can hide.
There is no universal winner. A thinner wire may improve slot fill but become harder to handle. A heavier insulation layer may increase durability while reducing available copper space. That trade-off deserves a real prototype. My own judgment would remain cautious until the wire survives electrical, mechanical, and environmental testing under expected conditions. Cost should follow performance, not replace it.
What Is the Best Enameled Aluminum Magnet Wire Type in 2026?
The best type depends on temperature, winding tension, and chemical exposure. IEC 60317-0-3:2020 and NEMA MW 1000-2024 recognize insulation systems around 155°C, 180°C, 200°C, and 220°C. Polyester insulation suits cost-sensitive motors with moderate heat. Polyesterimide offers better thermal endurance and stronger resistance to winding stress. Polyamide-imide overcoats usually provide superior abrasion resistance and support higher temperature classes. Polyurethane remains useful where direct solderability matters. However, its thermal and chemical limits require careful checking.
For high-temperature traction motors, composite polyesterimide/polyamide-imide systems often provide the most balanced performance. Their smooth enamel surface helps aluminum wire pass through tight slots. The softer aluminum core still needs controlled tension. Excessive pulling can stretch the conductor and damage insulation. Polyimide systems tolerate severe heat, but their higher cost may not suit ordinary industrial motors. A neat laboratory result cannot replace production testing. I would verify flexibility after aging, not only initial breakdown voltage.
Tips: Match the insulation class with the winding hot-spot temperature, not the average coil temperature. Request thermal-aging, abrasion, refrigerant, and voltage-withstand data from the supplier. Check conductor diameter after stripping. Small dimensional changes can alter slot fill and winding resistance. The 2024 NEMA data framework is useful, but actual motor geometry still decides reliability. That is where many selections become less certain.
| Insulation type | Typical thermal class | Typical maximum operating temperature | Solderability | Flexibility and abrasion resistance | Chemical and moisture resistance | Relative cost | Best-fit applications | Overall suitability for aluminum magnet wire |
|---|---|---|---|---|---|---|---|---|
| Polyester (PE) | Class 130 | Up to about 130°C | Poor; insulation normally requires mechanical or thermal removal | Good flexibility; moderate abrasion resistance | Moderate moisture and solvent resistance | Low | General-purpose motors, transformers, relays, and low-to-moderate temperature windings | Economical for cost-sensitive designs, but its thermal margin is limited for compact, high-load aluminum windings. |
| Polyester-imide (PEI) | Class 155 or 180 | About 155–180°C, depending on construction | Poor to limited; stripping is generally required | Good flexibility; good thermal-abrasion balance | Good resistance to oils, refrigerants, and many solvents | Medium | Industrial motors, generators, transformers, and automotive electrical systems | A strong general-purpose choice when higher thermal endurance and durability are required. |
| Polyester-imide with polyamide-imide overcoat (PEI/PAI) | Class 180 or 200 | About 180–200°C, depending on grade and test system | Poor; requires controlled stripping or termination preparation | Very good abrasion, scrape, and winding resistance | Very good resistance to oils, refrigerants, solvents, and moisture | Medium-high | Traction motors, compressors, electric vehicle drives, high-density motors, and demanding industrial equipment | Best all-around option for many 2026 aluminum winding designs because it combines high thermal endurance with strong mechanical protection. |
| Polyurethane (PU) | Class 130 or 155 | About 130–155°C, depending on grade | Good; many grades can be soldered without complete mechanical stripping | Excellent flexibility; moderate abrasion resistance | Moderate; performance can be affected by heat, humidity, and aggressive chemicals | Low-medium | Small transformers, coils, relays, inductors, and windings requiring simplified termination | Best when solderable termination and easy processing are more important than maximum thermal or chemical endurance. |
| Polyimide (PI) | Class 200 or higher | About 200°C and above, subject to the insulation system | Poor; specialized stripping and termination processes are normally needed | Good thermal stability; flexibility depends on film or coating construction | Excellent high-temperature and radiation resistance; verify moisture performance for each system | High | Aerospace equipment, high-temperature motors, specialty transformers, and space-limited windings | Best for extreme-temperature environments, but its higher cost and difficult termination make it excessive for ordinary applications. |
| Bondable enamel system | Usually Class 130–180 | Determined by the base enamel and bonding layer | Usually poor; bonding layer is not intended as a solderable finish | Good coil integrity after heat or solvent bonding; winding flexibility varies | Depends on the base enamel and bonding resin | Medium-high | Self-supporting coils, compact inductors, small motors, and vibration-sensitive assemblies | Useful where dimensional stability and coil bonding are critical, but it is selected by construction requirements rather than temperature rating alone. |
The best wire depends on temperature, voltage stress, winding space, and termination method. Aluminum weighs about one-third as much as copper, but its conductivity is only about 61% IACS. Designers usually need a larger conductor. That changes slot fill and winding geometry.
For traction motors, polyesterimide insulation with a polyamide-imide overcoat is a practical choice. It can offer strong thermal endurance and better resistance to inverter-related voltage stress. The International Energy Agency reported more than 17 million electric cars sold globally in 2024, exceeding one-fifth of total car sales. This growth increases demand for compact, efficient motor windings.
For transformers, rectangular enameled aluminum wire can improve space use and reduce lifting weight. However, engineers must control joint quality, oxidation, and thermal expansion. U.S. Department of Energy transformer analyses continue to emphasize efficiency, lifecycle cost, and material selection. A wire that looks economical may create expensive production problems.
Tips: Match the insulation class with the complete insulation system, not the wire alone. Check IEC 60317 requirements and UL 1446 system data where applicable. Use corona-resistant insulation for high-frequency drives. Confirm stripping, crimping, or welding settings on real production samples. I still prefer testing before approval; published ratings cannot predict every slot, varnish, or cooling condition. Small details matter.
Start with the winding design, not the product label. Measure the required current, operating voltage, coil space, and expected temperature. Aluminum carries less current than copper at the same diameter. A larger conductor may be necessary. Check the wire’s diameter tolerance and insulation thickness against your winding slot. Small errors can create pressure points or reduce the number of turns.
Next, choose the enamel insulation class for the real thermal environment. Do not select only by the motor’s normal temperature. Include heat from nearby cores, overload cycles, and poor ventilation. Review thermal endurance, voltage resistance, flexibility, and bondability in the technical data. For high-speed winding, test the insulation after bending and tensioning. A clean surface matters. Scratches can become failure points.
Connection quality deserves equal attention. Aluminum forms an oxide layer quickly, so terminals and joining methods must suit aluminum conductors. Verify contact resistance after thermal cycling. Test sample coils for insulation resistance, dielectric strength, and temperature rise. I once selected wire by price and nominal diameter alone. The winding looked acceptable, but its resistance exceeded the design target. That mistake taught me to compare finished coil performance, not just catalog figures. A short production trial is often more reliable than a perfect spreadsheet.
: It is an aluminum conductor covered with thin electrical insulation. The aluminum carries current. The enamel prevents contact between neighboring turns inside coils, motors, and transformers.
The structure usually includes an aluminum core and an enamel coating. Some versions add a protective or bonding topcoat. That extra layer can improve abrasion resistance and help hold a heated coil shape.
Aluminum weighs about one-third as much as copper. This can reduce lifting effort and equipment weight. Its conductivity is lower, near 61% IACS, so designers need a larger conductor. That trade-off is easy to underestimate.
Polyester insulation can suit cost-sensitive motors with moderate heat. Polyesterimide offers stronger thermal endurance and better winding-stress resistance. A polyamide-imide overcoat usually improves abrasion protection. The cheapest option is not always the easiest to produce.
A composite polyesterimide and polyamide-imide system often provides balanced performance. It can tolerate heat, tight winding paths, and mechanical rubbing. The aluminum core still needs controlled tension. Too much pulling may stretch the wire or damage its coating.
Rectangular wire can improve slot utilization in transformers and compact motors. Round wire is often easier to guide through winding paths. The better shape depends on slot geometry, bending limits, and termination methods. A drawing alone cannot confirm production suitability.
Test resistance, dielectric strength, flexibility, thermal aging, and coating adhesion. Also check abrasion, refrigerant exposure, and voltage withstand when relevant. Measure the conductor after stripping. Small dimensional changes can alter slot fill and winding resistance.
Control winding tension, stripping settings, crimping, welding, and joint quality. Aluminum oxidation can complicate electrical connections. Thermal expansion also deserves attention. I would test real production samples, not only trust published ratings. That judgment may still need revision.
Choosing the best Enameled Aluminum Magnet Wire in 2026 requires more than comparing conductor size. This wire consists of an aluminum conductor covered by a thin enamel insulation layer, combining low weight, good electrical conductivity, and efficient heat dissipation. The ideal type should be evaluated by insulation temperature rating, dielectric strength, flexibility, thermal endurance, winding performance, resistance to abrasion, and compatibility with varnishes or other insulating materials. These factors determine reliability, energy efficiency, manufacturing ease, and service life.
Different enamel systems offer distinct advantages, from general-purpose insulation to options designed for higher temperatures, improved mechanical durability, or enhanced chemical resistance. Motor windings may prioritize flexibility and thermal stability, while transformers often require strong dielectric performance and dependable insulation under continuous electrical stress. Other applications may focus on compact winding, reduced weight, or resistance to vibration. A practical selection process should begin by defining operating temperature, voltage, winding method, space limitations, environmental conditions, and compliance requirements, then comparing wire types against these needs before finalizing the most suitable specification.